
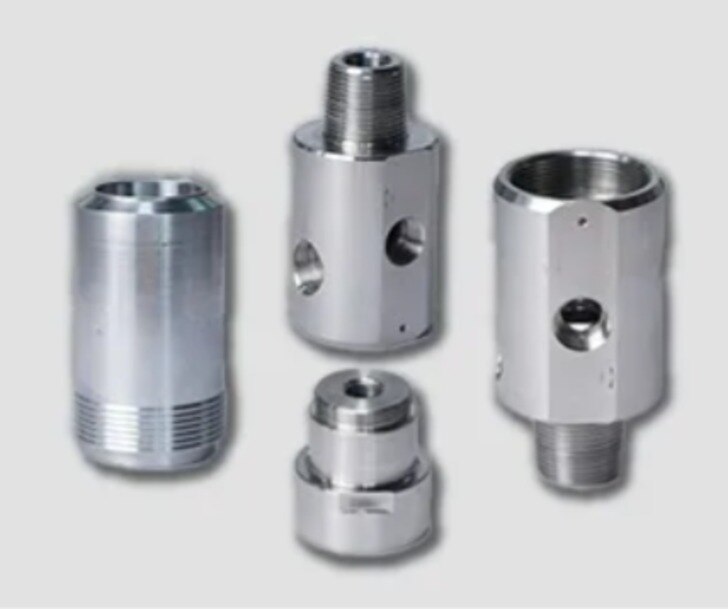
A quotation for a machined component is only as reliable as the information behind it. Missing drawing controls, material conditions, thread details or inspection rules can produce parts that meet a supplier’s interpretation but fail in your assembly. Use the checklist below to define the part, select the machining process and agree how conformity will be proved before you place an order.
Key takeaways
- Include revision, units, quantity, annual volume, delivery, and packaging in every RFQ.
- Specify material grade, temper, hardness, heat treatment, and coating requirements.
- Review pockets, holes, wall thickness, and tolerances for manufacturability before approval.
- Define inspection reports, sampling, certificates, and acceptance criteria before production starts.
Build an RFQ drawing that leaves no critical field open
An accurate quote needs a complete drawing and RFQ, not “machine to print.” State the part number, drawing revision, units, projection method, quantity, annual volume, delivery target, and packaging requirement. Unspecified limits become both pricing assumptions and acceptance disputes.
1. Define the component and material. Name the exact grade, product form, temper or hardness, heat treatment, and required certificate, such as EN 10204 3.1. Add lot, heat or cast-number traceability and positive material identification when pressure, corrosion, or traceability matters.
2. Define the machining. Show the datum reference frame, general tolerances, individually toleranced dimensions, GD&T, surface roughness, edge breaks, burr limits, and critical-to-function features. Identify the machining envelope, deep pockets, thin walls, narrow slots, minimum internal radii, fixture holes, and workholding access.
State whether the supplier may use 3+2 positioning or simultaneous five-axis machining, and which faces establish manufacturing datums.
3. Define threads and downstream processes. Specify thread standard, nominal size, pitch, class or fit, depth, incomplete-thread relief, start chamfer, cutting or forming method, and functional gauging. For passivation, plating, anodizing, coating, electropolishing, or heat treatment, state the process specification, masked surfaces, allowable thickness or growth, and whether inspection occurs before or after processing.
4. Define acceptance. State first-article inspection, lot reports, sampling or 100% inspection, test requirements, certificates, and packaging. This CNC component order checklist is the practical CNC VMC component specifications before ordering record: every open field becomes a supplier question before release.
Match the component to the right machining process and material condition
A hardened steel bar, a slender stainless pin and a cast aluminium block do not belong on the same machine. Match the process to the material condition and geometry before requesting a price; otherwise tooling, workholding and secondary operations will distort the quote.
1. Choose conventional turning for rotational parts with a diameter large enough for a chuck or collet, especially when the profile needs facing, grooving, threading or boring. Machine annealed or normalized stock before heat treatment, then leave grinding or hard turning allowance if the final diameter is critical.
2. Choose sliding-head machining for small, long parts with a high length-to-diameter ratio. The guide bushing supports the material beside the cutting tool, improving concentricity on slender pins, valve stems and stepped shafts. State bar diameter, roundness, remnant length and cutoff allowance in the cnc precision component specifications.
3. Choose a VMC for prismatic parts requiring pockets, drilled patterns, side features or broad planar faces. Confirm the VMC component requirements against the material’s condition: soft aluminium and annealed steel cut efficiently, while hardened material demands suitable carbide tooling, rigidity and slower metal removal.
4. Choose mill-turn machining when one setup must combine accurate turning with cross-holes, milled flats, angled features or multiple face orientations. It reduces datum-transfer error, but complex programming and live-tool access can increase cost.
Specify whether heat treatment, plating, passivation or coating occurs before or after final machining. Inspection timing, masking surfaces and permitted dimensional growth prevent a finished coating from making a previously correct part rejectable.
Check manufacturability before approving pockets, holes and thin features
A pocket that fits the cutter can still be impossible to machine reliably. Confirm whether every feature is reachable in one setup, which surfaces establish the manufacturing datums, and whether the supplier will use 3+2 positioning or simultaneous five-axis machining. Otherwise, features that meet their individual dimensions can be misaligned across faces.
Your cnc vmc component for specifications before ordering review must answer these physical and workholding questions:
- Can the machine reach every pocket, hole, slot and face without tool or spindle interference?
- Do deep pockets need a long tool, and does that create chatter, deflection or unacceptable corner radii?
- Are thin walls, narrow slots or small internal radii strong enough to survive cutting and clamping?
- Can the fixture expose all critical surfaces, or will a second setup be necessary?
- Are fixture holes, soft jaws, locating pads or sacrificial stock permitted in non-functional areas?
- What unsupported length, straightness or runout applies to slender features?
- Are clamping marks prohibited, and may the supplier use a tailstock, steady rest or secondary support?
| Machining arrangement | Main risk | Confirm before approval |
|---|---|---|
| One setup | Limited access to hidden faces | Datum surfaces and tool clearance |
| 3+2 positioning | Setup-to-setup alignment error | Angular access and positional tolerances |
| Simultaneous five-axis | Higher programming and inspection complexity | Required surface accuracy and inspection method |
These checks define the vmc component requirements that determine whether the drawing describes a stable process or only a theoretical shape. Reject a design that depends on unsupported walls or inaccessible datums.
Separate functional tolerances from cosmetic and non-critical requirements
Put every requirement into one of two groups: characteristics that control assembly, sealing, strength or motion, and appearance requirements that do not affect performance. Mark the first group as critical-to-function on the drawing; otherwise a supplier may apply the same inspection effort to a hidden face and a sealing diameter.
- Define the datum reference frame with primary, secondary and tertiary datums, and attach each critical dimension to its actual locating surfaces.
- Apply GD&T symbols for position, perpendicularity, flatness, runout or profile, with tolerance zones and datum references; do not rely on a tight ± dimension to control form and location.
- Specify each thread’s standard, nominal size, pitch, class or fit, depth, relief and start chamfer. State whether it is cut or formed and require a functional plug or ring gauge when mating fit matters.
- Give surface finish as a measured Ra or Rz value, identify the faces and measurement direction, and state whether inspection occurs before or after plating, anodizing, passivation or coating.
- State edge-break limits such as 0.2–0.4 mm, and define burr acceptance by maximum height, prohibited locations and inspection method.
Keep cosmetic notes separate: identify visible faces, allowable marks, colour variation and handling scratches without imposing those limits on functional surfaces. A note such as “break all edges” cannot replace a burr limit.
Your CNC precision component specifications and cnc component order checklist should name the instrument or gauge, datum simulation, measurement points and inspection stage. For valve parts, add pressure-boundary, seat or shell leakage criteria separately; dimensional conformity alone does not prove sealing performance.
Agree inspection evidence, processing steps and supplier capability
Before releasing the purchase order, make the inspection record, finishing route and packing method acceptance criteria—not informal supplier assumptions. Your cnc vmc component for specifications before ordering package must identify what is measured, when it is measured and how the parts arrive.
- Specify first-article inspection, a dimensional report for every lot, sampling or 100% inspection, and the critical-to-function characteristics. Name the measurement method: CMM, optical system, air gauge, plug gauge, roundness tester or standard micrometer, including datum simulation, measurement points, gauge resolution and calibration status.
- Require material traceability and an EN 10204 3.1 certificate where applicable. Record the drawing revision, lot number, operator or inspector, equipment identification and nonconformance disposition.
- State every post-machining process by specification: heat treatment hardness and cycle, passivation, plating, anodizing, coating or electropolishing. Define masking, allowable coating thickness, dimensional growth, surface roughness, colour limits and whether inspection occurs before or after treatment.
- Define threads completely: standard, nominal size, pitch, class or fit, depth, relief, start chamfer and whether they are cut, formed or rolled. State whether acceptance uses a functional plug gauge or dimensional measurement.
- Specify packaging: clean and dry parts, individual wrapping or separators, thread caps, VCI paper or desiccant, carton quantity, lot labels and protection against impact, corrosion and mixing revisions.
Ask whether the VMC component fits one setup, needs 3+2 or simultaneous five-axis machining, and which surfaces establish manufacturing datums. Efficient Precision & System Pvt.Ltd should also identify its inspection equipment, subcontracted treatments and capacity before you commit the order. A cnc component order checklist prevents those answers from arriving after production starts.
Frequently asked questions
What information must a CNC VMC component RFQ include?
State the part number, drawing revision, units, projection method, quantity, annual volume, delivery target, packaging, material, finishes, tolerances, and inspection requirements.
How do you match a component to the right machining process?
Compare the material condition, feature geometry, part size, tolerance requirements, production volume, and required operations before choosing VMC, turning, or multi-axis machining.
Which CNC component features require a manufacturability review?
Review deep pockets, small or intersecting holes, thin walls, narrow slots, internal corners, difficult tool access, and tight tolerances before approving the drawing.
How should buyers separate functional and cosmetic requirements?
Mark datums, fits, sealing surfaces, threads, and critical dimensions as functional; define cosmetic limits separately for marks, burrs, discoloration, and surface appearance.
What inspection evidence should buyers request from a CNC supplier?
Agree the measurement method, sampling plan, first-article report, material certificate, heat-treatment records, coating records, and capability evidence before production.